Engineered to seal,
The last line of defense against leakage
+86-13566064802

Views: 0 Author: Site Editor Publish Time: 2026-10-12 Origin: Site
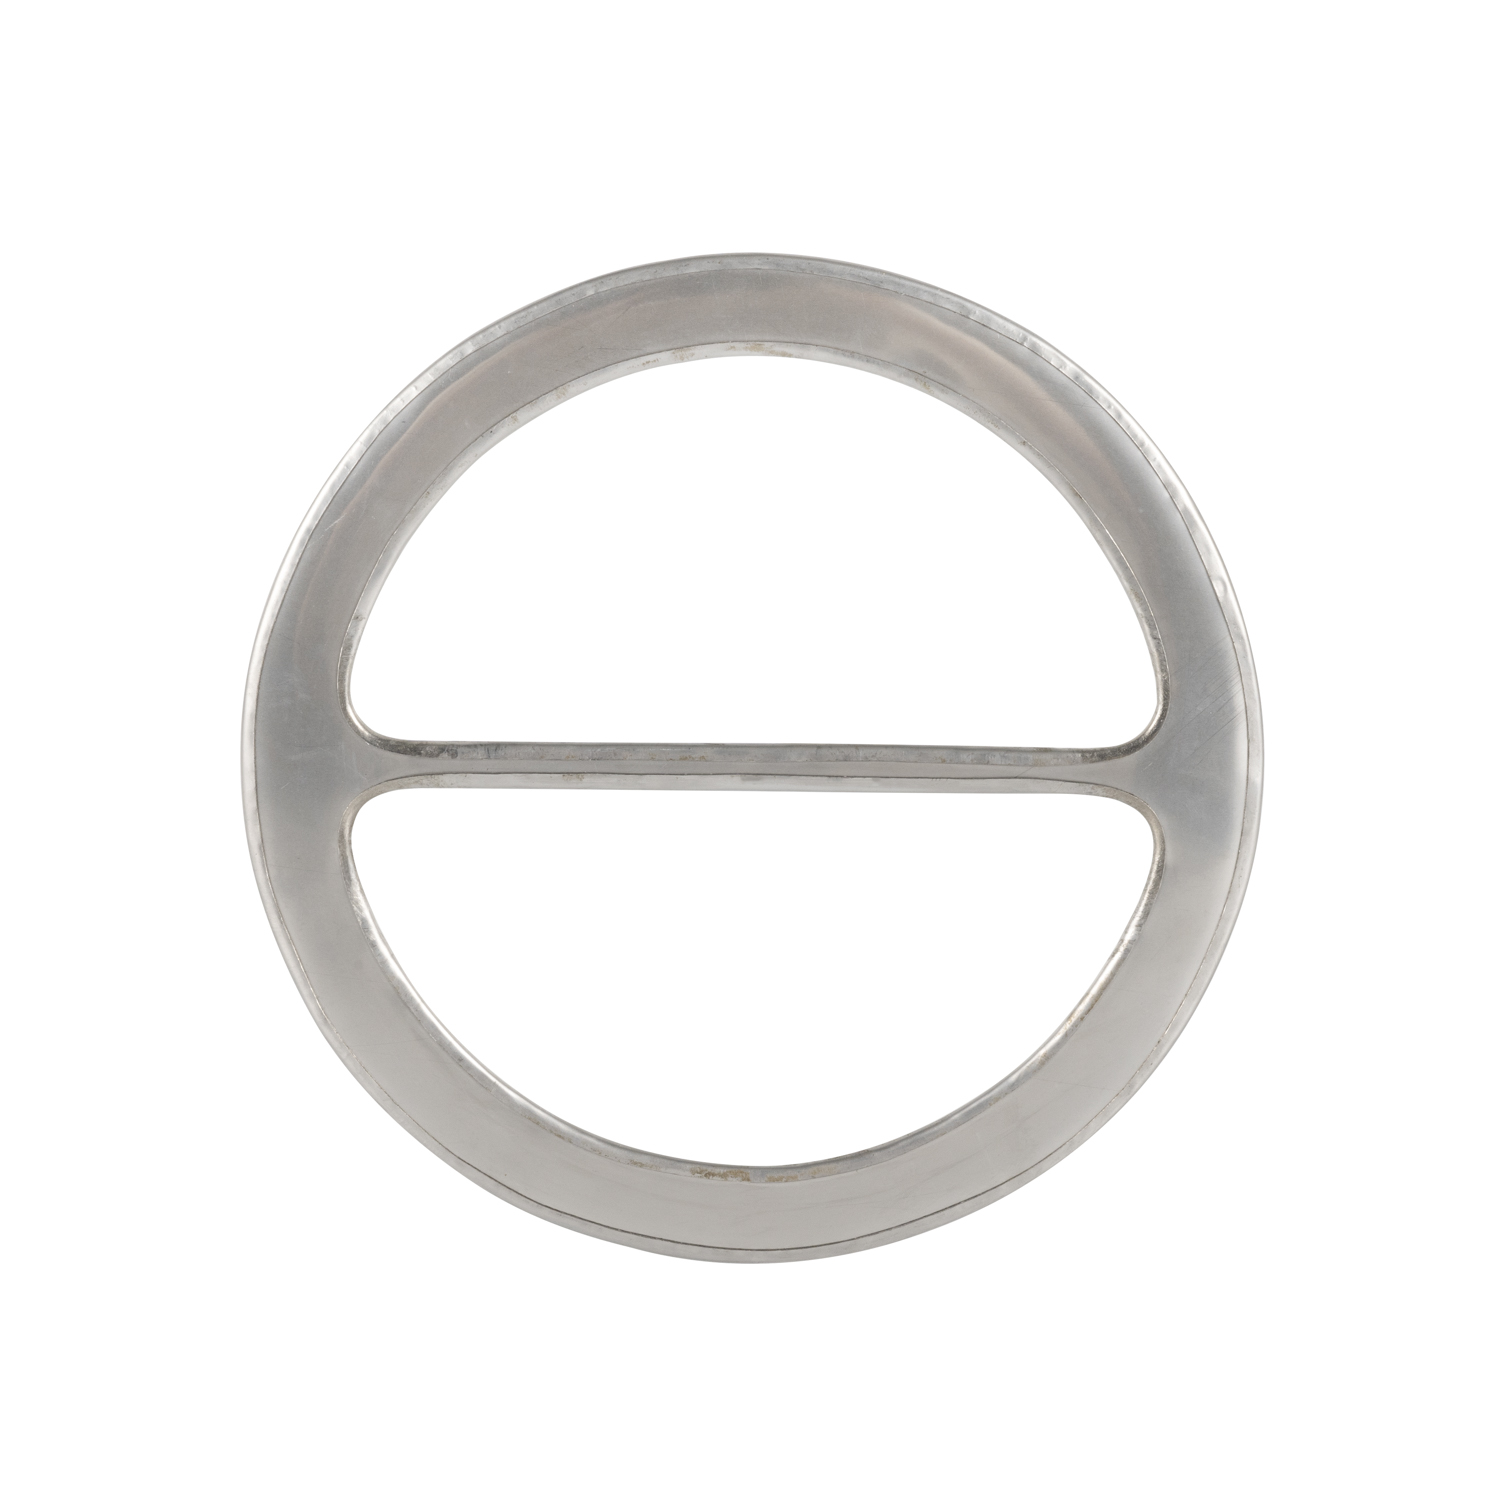
A Heat Exchanger Gasket Blowout represents a severe failure in industrial fluid systems. When a seal ruptures under pressure, the consequences cascade rapidly throughout the facility. Plant operators face unplanned operational downtime, immediate safety hazards, and sudden spikes in energy consumption. Environmental remediation becomes necessary when hazardous process fluids escape containment. Shell and tube heat exchangers carry inherent mechanical vulnerabilities. Thermal cycling, pressure surges, tube sheet welding stress, and aggressive media place immense stress on flanged joints. Shifting from reactive leak repair to proactive engineering controls is essential for plant reliability. Preventing joint failure requires a strict combination of precise material selection, rigorous installation protocols, and unwavering operational discipline. This guide details the technical mechanics behind seal failures and outlines concrete steps to maintain flanged joint integrity.
Material Compatibility Dictates Lifespan: Selecting the correct Heat Exchanger Gasket requires matching material properties against the exact chemical composition, peak temperatures, and pressure ratings of the process fluid.
Installation Precision Prevents Failure: Uneven bolt loads, improper torquing, and flange surface contamination (e.g., sand, iron filings, grease) are the leading preventable causes of joint failure.
Operational Controls are Non-Negotiable: Managing flow rates, mitigating fouling, and standardizing startup/shutdown procedures are critical to minimizing thermal shock and pressure spikes.
Table of Contents
Heat-exchanger gasket failure occurs when sealing performance is compromised by insufficient bolt load, thermal stress, pressure fluctuations, or mechanical deformation. Minor leakage may develop gradually, while a gasket blowout causes sudden loss of containment. Identifying these failure mechanisms helps prevent equipment damage and unplanned shutdowns.
Thermal cycling and differential expansion can reduce gasket compression and cause flange leakage. Different materials expand at different rates, while welding stress and damaged expansion joints may contribute to flange distortion. Selecting gaskets with suitable recovery properties and controlling temperature changes helps maintain sealing integrity.
Material | Thermal Expansion (×10⁻⁶ in/in/°F) | Sealing Consideration |
|---|---|---|
Carbon Steel | 6.5 | Moderate thermal expansion |
304 Stainless Steel | 9.6 | Higher expansion may affect gasket compression |
316 Stainless Steel | 8.9 | Requires consideration of thermal movement |
Titanium | 4.8 | Differential expansion with stainless steel |
Values are approximate reference figures and may vary with temperature and material grade.
Pressure surges, water hammer, and excessive flow rates can overload heat-exchanger gasketed joints. Plugging damaged tubes reduces available flow area, potentially increasing fluid velocity and differential pressure. Proper flow control, gradual valve operation, and engineering assessment of tube plugging limits help prevent excessive joint stress and gasket failure.
Heat-exchanger fouling occurs when scale, sludge, or biological deposits accumulate inside tubes, restricting flow and reducing heat transfer efficiency. Increased flow resistance may raise differential pressure and place additional stress on gasketed connections. Regular cleaning, water treatment, and pressure monitoring help control fouling and reduce sealing failure risks.
Heat-exchanger gasket selection depends on operating temperature, pressure, chemical compatibility, and flange conditions. Choosing the appropriate material helps prevent leakage, reduce maintenance costs, and improve equipment reliability.
Temperature and chemical compatibility are essential when selecting heat-exchanger gaskets. Engineers must consider process fluid composition, pH, operating temperature, and potential corrosion risks. Materials such as NBR, graphite, and stainless steel offer different resistance characteristics. Selecting compatible gasket components helps prevent chemical degradation and premature sealing failure.
Different gasket constructions provide distinct advantages depending on pressure, temperature, and flange requirements.
Gasket Type | Key Advantages | Suitable Applications |
|---|---|---|
Elastomeric | High compressibility, low seating stress | Low-pressure water and utility systems |
Semi-Metallic | Good strength and thermal cycling resistance | Industrial heat exchangers, steam systems |
Solid Metallic | High-pressure and high-temperature capability | Severe industrial operating conditions |
Gasket material grade directly influences sealing reliability and service life. Premium materials such as 316 stainless steel, Inconel, Monel, and flexible graphite offer improved resistance to demanding temperatures and chemical environments. Selecting suitable materials helps reduce corrosion, gasket relaxation, and unplanned maintenance.
Proper heat-exchanger operation helps maintain flange sealing integrity and prevent premature gasket failure. Controlling flow, pressure, temperature changes, and fouling reduces mechanical stress on gasketed connections.
Flow rate and differential pressure control help prevent excessive mechanical loading in heat exchangers. Pressure transmitters, control valves, and variable frequency drives (VFDs) support stable fluid circulation and reduce sudden pressure fluctuations. Regular monitoring helps identify restrictions and maintain safe operating conditions.
Fouling prevention helps maintain efficient heat transfer and stable pressure conditions. Appropriate water treatment, chemical cleaning, and mechanical cleaning can reduce scale, biological growth, and internal deposits. Regular maintenance prevents excessive pressure drops and supports long-term gasket reliability.
Controlled startup and shutdown procedures reduce thermal shock and protect heat-exchanger gaskets from sudden expansion and contraction. Operators should verify valve positions, vent trapped gases, introduce process fluids in the specified sequence, and gradually adjust temperatures while monitoring pressure. Heating and cooling rates must follow equipment manufacturer requirements.
Correct gasket installation requires clean flange surfaces, uniform bolt loading, and appropriate pressure testing. Standardized maintenance procedures help prevent leakage and extend heat-exchanger service life.
Flange surface preparation is essential for reliable gasket sealing. Remove old gasket material, corrosion, and debris before installation. Inspect flange faces for scratches, pitting, and deformation, and verify that surface roughness matches the selected gasket manufacturer's requirements.
Gasket Type | Flange Surface Finish (Ra, μin) |
|---|---|
Elastomeric (Rubber) | 250–500 |
Spiral Wound | 125–250 |
Kammprofile | 125–250 |
Solid Metal Ring Joint | 63 maximum |
These are reference values from the supplied material; actual requirements depend on gasket design, flange type, and manufacturer specifications.
Proper bolt tightening ensures uniform gasket compression and prevents flange leakage. Use calibrated torque tools, suitable thread lubrication, and a cross-pattern tightening sequence with progressive torque stages. Final bolt loads must meet gasket and flange specifications to prevent both under-compression and gasket damage.
Hydrostatic testing verifies heat-exchanger sealing integrity before commissioning. Technicians should isolate the equipment, remove trapped air, and apply the approved test pressure according to the applicable procedure. Floating-head exchangers also require inspection of internal seals, test rings, and retaining components. After testing, drain and dry the system as required to prevent corrosion.
Preventing a flanged joint failure requires a comprehensive, proactive strategy. Relying solely on reactive maintenance leads to dangerous leaks and severe operational disruptions. Success depends on understanding the mechanical forces at play and implementing strict engineering controls. Facilities must prioritize precision during every phase of operation and maintenance.
Take the following actionable steps to secure your fluid systems:
Schedule a comprehensive flange management audit for all critical heat exchangers.
Review and update current startup and shutdown standard operating procedures to eliminate thermal shock.
Implement continuous differential pressure monitoring to detect early signs of severe tube fouling.
Mandate the use of calibrated torque wrenches and strict tightening sequences for all maintenance turnarounds.
A: The most frequent causes include uneven bolt load during installation, severe thermal shock during startup, improper material selection for the process fluid, and unmitigated internal fouling that drives up internal system pressure.
A: Correct torque calculations rely on the specific gasket factor (m), the minimum seating stress (y), maximum internal operating pressure, and the yield strength of the selected bolts. Engineers use these variables to determine the exact compressive load required.
A: Yes. Internal fouling restricts fluid flow, which significantly increases the pressure drop across the unit. This restriction forces internal hydraulic pressure to spike, placing excessive mechanical stress on the flanged joint until it ruptures.
A: Blocking a large number of leaking tubes decreases the available cross-sectional flow area. This artificially increases the fluid velocity and internal pressure in the remaining open pipes, severely stressing the flanged connection.
A: Spiral wound profiles act like a spring, offering excellent recovery during thermal cycling. Kammprofiles feature a solid grooved metal core with a soft facing, providing superior blowout resistance and requiring less seating stress than solid metal rings.
A: These seals must be replaced during every maintenance turnaround or anytime the flanged joint is opened. They permanently deform during initial compression and are strictly non-reusable.
A: Semi-metallic profiles generally require a flange surface finish between 125 and 250 microinches RMS. The surface must also be completely free of sand, iron filings, grease, and old sealing material to function correctly.